Summary: Warehouse layout engineering decisions happen months before operations begin, locking in labor efficiency, pick path speed, and throughput capacity for years. Four variables drive every flow pattern choice. Inbound/outbound ratios, SKU velocity distribution, order profile characteristics, and physical building constraints. High-SKU catalogs face compounding complexity that requires three-dimensional slotting strategies and replenishment paths designed before racking goes up. Every flow pattern solves one problem by creating another, and the right choice depends on which trade-offs your operation can absorb. When evaluating a 3PL, the productive questions focus on how they determined slotting methodology for your SKU profile and what drove their flow pattern selection. The answers reveal whether their infrastructure was engineered for operations like yours.
When a brand executive tours a 3PL facility, they see racks stretching toward the ceiling, conveyors humming with cartons, and dock doors cycling through trailer after trailer.
What they rarely see is the engineering logic that determined why every element sits precisely where it does.
The Layout Decisions Lock In Years Before the First Pallet Arrives
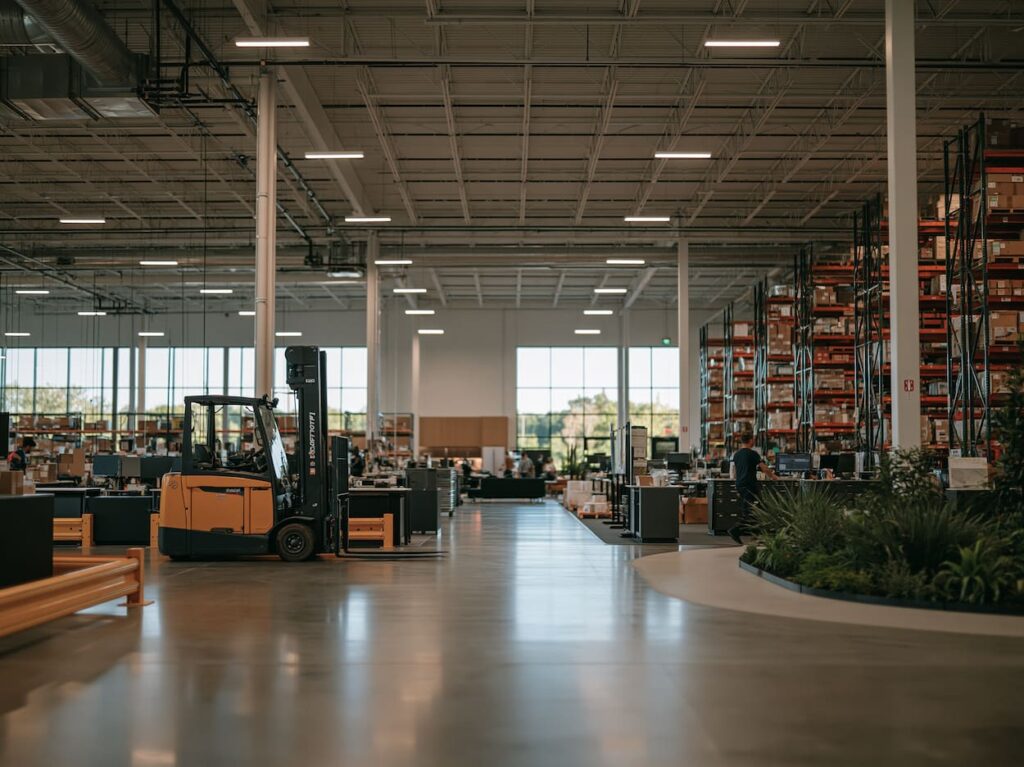
Warehouse layout is applied physics, constrained optimization, and predictive modeling compressed into a floor plan that will govern operational costs for years.
The decisions that matter most happen months before the first pallet arrives. Rack placement, zone boundaries, conveyor routing, and dock door allocation are locked in when permits are pulled and concrete is poured.
Changing them later means tearing out infrastructure, halting operations, and absorbing costs that compound across every order touched during the transition.
This creates a core tension that 3PLs navigate constantly. A layout must simultaneously optimize for receiving velocity, storage density, pick efficiency, and shipping throughput. These goals conflict.
Maximizing storage density means tighter aisles, which slows pick travel. Prioritizing receiving speed means dedicating dock doors and staging area that could otherwise serve outbound shipments. Every layout represents a series of calculated trade-offs, and the quality of those calculations determines whether a facility runs at 94% labor efficiency or 71%.
Industry benchmarks reinforce this gap. According to research from the Warehousing Education and Research Council (WERC), top-tier “Class A” distribution centers leverage precise floor-plan engineering to consistently maintain order accuracy rates above 99.8% while cutting travel time (which accounts for up to 50% of total picking labor) in half.
The question for any brand evaluating outsourced warehousing and fulfillment services is whether they engineered that space for operations that match yours.
Four Variables Constrain Every Flow Pattern Decision
Before a 3PL commits to U-shaped, straight-through, or L-shaped flow configurations, they analyze a set of upstream variables that most brands never think to ask about.
Inbound and Outbound Ratios Determine Whether Receiving or Shipping Gets Priority
The fundamental architecture follows from this ratio. A facility receiving four truckloads daily but shipping 4,000 individual parcel orders operates under different physics than a facility receiving 400 inbound pallets and shipping 40 full truckloads.
The first scenario demands minimal receiving footprint and maximum pick-and-pack infrastructure. The second demands the inverse. Misreading this ratio means either receiving backs up into the parking lot or shipping lanes sit empty while pickers wait for replenishment.
SKU Velocity Distribution Dictates How Much Prime Space Goes to Fast Movers
In a typical catalog, roughly 20% of SKUs generate 80% of movement. Some operations skew even harder toward concentration, with 10% of SKUs driving 90% of picks.
This distribution dictates how much prime real estate goes to fast-movers in ergonomic golden-zone pick faces versus how much gets allocated to reserve storage for the long tail. A layout that treats all SKUs equally wastes travel time on every order.
Single-SKU Bulk Orders and Multi-SKU Each-Picks Require Different Pick Paths
Order profile characteristics drive this logic. Bulk orders flowing to retail replenishment move through a facility differently than multi-SKU each-pick orders shipping direct to consumers. Bulk orders benefit from case-pick zones with wide aisles and forklift access.
Each-pick operations need dense forward pick faces with walking paths optimized for 15 to 25 SKU touches per order. A layout optimized for one profile creates friction when processing the other.
Physical Dock Door Placement Often Overrides Flow Preference Entirely
The building footprint determines how many dock doors exist and where they sit.
A facility with doors clustered on one wall cannot run a true straight-through flow regardless of what the operation might prefer. Physical limitations frequently dictate layout more than operational philosophy.
Once these variables are mapped, the 3PL selects a flow pattern. But for high-SKU operations typical of brands outsourcing fulfillment, another layer of complexity compounds every decision.
What Is Warehouse Flow Pattern Design?
Warehouse flow pattern design is the process of determining how inventory physically moves through a facility from receiving to shipping. It encompasses the sequencing of zones (receiving, storage, picking, packing, shipping), the directional paths that product and workers follow, and the infrastructure placement that enables or constrains that movement.
The three primary patterns are U-shaped flow (receiving and shipping on the same side), straight-through flow (receiving and shipping on opposite ends), and L-shaped or hybrid configurations that adapt to building constraints.
Effective flow pattern design minimizes travel distance, prevents congestion between competing activities, and aligns physical infrastructure with the specific velocity and order profile characteristics of the operation.
Simple Zone Logic Breaks When SKU Counts Reach the Thousands
A distributor moving 200 SKUs can use simple zone logic. Fast movers near shipping, slow movers in the back, a single pick path through the middle. The math stays manageable.
A brand with 20,000 active SKUs, seasonal rotation, kitting requirements, and unit dimensions ranging from jewelry pouches to furniture boxes cannot apply the same logic. SKU complexity multiplies every layout decision and exposes weaknesses that simpler operations never encounter.
Slotting Must Address Rack Level, Pick Face Width, and Replenishment Path Simultaneously
The question involves rack level, pick face width, shelf depth, and replenishment path.
A SKU selling 500 units monthly needs different pick face capacity than one selling 50 units. Get this wrong and fast movers stock out mid-shift while slow movers occupy prime real estate that should generate 10x the picks per hour.
Research indicates that order picking accounts for over 50% of total warehouse labor costs, with more than half of that time spent walking between pick faces rather than handling inventory.
SKUs Ordered Together Need Proximity but Velocity Wants Fast Movers Concentrated
These competing demands create the adjacency problem. SKUs frequently ordered together need physical proximity to minimize travel time per order. But velocity-based slotting wants the fastest movers concentrated in the tightest zone regardless of what they ship with.
A brand selling apparel might see size medium of a given style ship with size large 40% of the time, but medium sells 3x the volume of large. Pure velocity slotting separates them. Pure affinity slotting ignores velocity. Layout must reconcile both, and the reconciliation happens at the infrastructure level before dynamic slotting software ever runs.
Replenishment Flow Paths Must Be Designed Before Racking Goes Up
High-SKU operations cannot fit full inventory depth in pick faces.
They need reserve storage feeding those faces through replenishment cycles. The layout must account for replenishment travel paths that do not collide with active picking, staging zones where reserve inventory waits for putaway, and vertical flow between bulk storage levels and floor-level pick modules.
None of this is optional for complex catalogs. All of it must be designed before racking goes up.
These are decisions built into systems designed to flex as SKU counts grow and order profiles shift.
What Is SKU Slotting and Why Does It Matter?
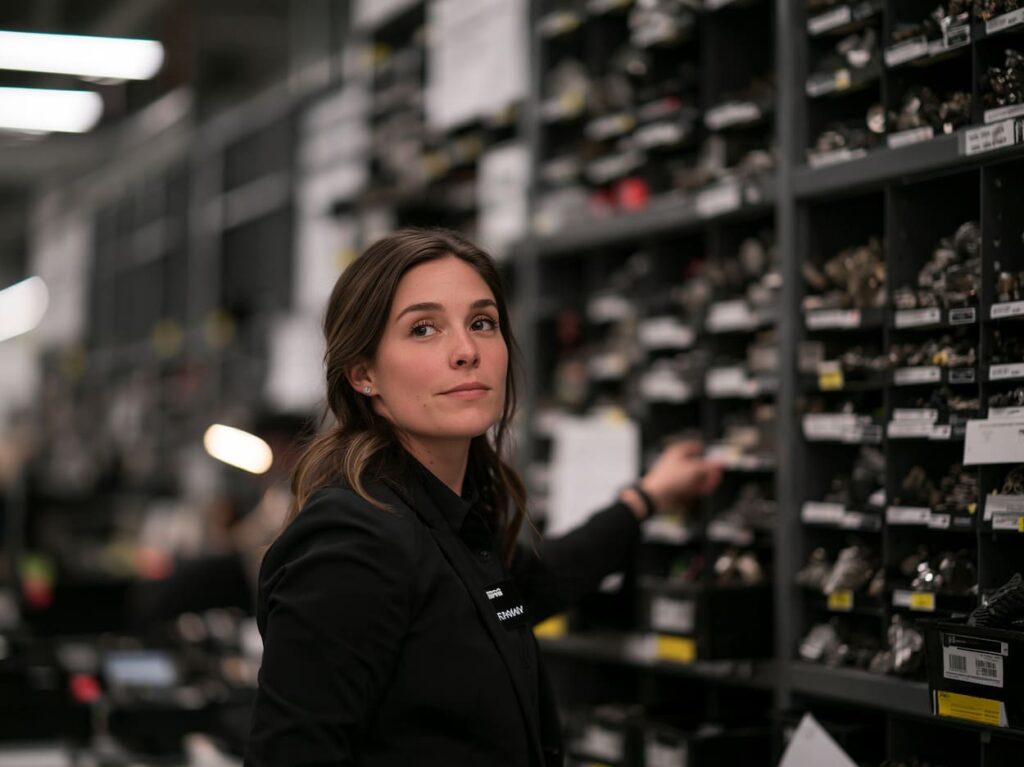
SKU slotting is the methodology for assigning each product to a specific storage location based on its velocity, physical dimensions, pick frequency, and relationship to other products.
It determines which items occupy prime ergonomic positions (waist-to-shoulder height in high-traffic pick zones) versus which get relegated to harder-to-reach reserve locations. Slotting matters because it directly controls picker travel time and efficiency. Poor slotting forces workers to walk farther, reach higher, and wait longer for replenishment.
Optimal slotting concentrates the fastest-moving 20% of SKUs in the most accessible 10% of pick face locations, dramatically reducing the distance traveled per order and increasing picks per labor hour.
Every Flow Pattern Solves One Problem by Creating Another
Brand catalogs do not stay static. SKU counts grow as product lines expand. Order profiles shift as channels evolve. Seasonality creates demand peaks that stress every layout assumption.
A facility designed purely for current-state optimization becomes a bottleneck 18 months later when the operation looks different than projected.
U-Shaped Layouts Let Labor Flex Between Inbound and Outbound Functions
This configuration routes product flow so that receiving and shipping share a building side, with storage and picking occupying the interior.
The consolidation enables labor to flex between inbound and outbound functions depending on where volume pressure sits at any given hour. When receiving trucks arrive in clusters, workers shift to unloading. When afternoon shipping cutoffs approach, the same workers move to packing stations.
For operations with variable volume and smaller teams, this flexibility reduces idle time and smooths labor planning.
Straight-Through Layouts Eliminate Congestion but Sacrifice Labor Flexibility
Separating inbound and outbound entirely places receiving at one end, shipping at the other, with product flowing linearly through storage and picking zones.
This separation eliminates congestion that occurs when inbound and outbound traffic compete for the same dock doors and staging areas. High-velocity operations with predictable daily flow benefit from this clarity. Forklifts moving receiving pallets never cross paths with pickers working outbound orders.
But the trade-off is labor cannot easily flex between functions separated by 400 feet of racking.
Hybrid Configurations Optimize Around Constraints That Neither Pure Model Handles
Irregular building footprints with dock doors on perpendicular walls cannot run straight-through flow.
Multi-client 3PL environments where different brands require physical separation need zone isolation that U-shaped consolidation does not provide. L-shaped and hybrid configurations optimize around constraints rather than ideals, and recognizing which constraints actually bind for a given operation is expertise unto itself.
The choice between patterns is never “which is best” in the abstract. The choice is “which constraints matter most for this operation, and which trade-offs are acceptable.”
A 3PL with experience across dozens of similar operations has seen which choices create regret and which hold up as brands scale.
What Is the Difference Between U-Shaped and Straight-Through Warehouse Flow?
U-shaped flow places receiving and shipping docks on the same side of the building, with product moving into storage, through picking zones, and back toward the shared dock area.
Straight-through flow places receiving at one end and shipping at the opposite end, with product moving linearly from inbound to outbound.
The key trade-off is flexibility versus separation. U-shaped layouts allow workers and equipment to shift easily between receiving and shipping tasks, which benefits operations with variable volume or limited staff.
Straight-through layouts physically separate inbound and outbound traffic, eliminating congestion and cross-traffic but requiring dedicated labor for each function. Neither is universally superior. The right choice depends on volume predictability, staffing model, and building constraints.
A 3PL’s 50th Layout Avoids Mistakes Their First Layout Made
A brand launching direct-to-consumer fulfillment encounters their warehouse layout problem for the first time.
They model their SKU velocity, project their order volumes, and make reasonable assumptions about how the operation will behave. Some of those assumptions will prove wrong.
Demand will concentrate differently than expected. SKU counts will grow faster in some categories and slower in others. Order profiles will shift as marketing channels evolve.
A 3PL running similar operations for dozens of brands has already seen these patterns play out. They have watched SKU proliferation stress slotting logic that seemed adequate at launch. They have observed order profile shifts expose pick path inefficiencies that did not exist in year one.
They have measured exactly how much labor cost increases when forward pick replenishment was under-designed.
This pattern recognition compounds across every client engagement.
A 3PL designing their 50th high-SKU ecommerce layout draws on failure modes they prevented for clients 12 through 49. A brand designing their first layout cannot access that learning. They pay for it through trial and error, absorbing the cost in labor inefficiency, mis-ships, and throughput constraints they did not anticipate.
The expertise gap shows up in decisions most brands would never think to make. 3PLs pre-engineer for problems their clients have not yet encountered. Reverse logistics zones sized for return rates that spike in Q1.
Designing dedicated areas for custom kitting and assembly services positioned to pull seamlessly from high-affinity SKU clusters. Hazmat isolation that satisfies fire code without fragmenting pick paths. Lot-code rotation flows that ensure FIFO compliance without manual oversight.
None of these features appear on a capability checklist. All of them determine whether an operation runs smoothly at scale or accumulates friction that shows up as cost-per-order creep that seems impossible to diagnose.
The Questions That Reveal Whether a Facility Was Engineered for You
When evaluating a 3PL partnership, the visible facility tour reveals less than the invisible engineering beneath it. Square footage is a commodity.
Layout expertise is not.
The productive questions are the ones most brands never think to ask.
Questions to ask when evaluating a 3PL’s layout expertise:
- How do you determine slotting methodology for a catalog of our SKU count and velocity distribution?
- What drove your flow pattern selection for this facility, and how does it accommodate volume growth?
- How do you handle the transition when a brand’s SKU count doubles or order profile shifts from wholesale to direct-to-consumer?
- Where are replenishment paths routed relative to active pick zones?
- How is forward pick face capacity determined for high-velocity SKUs?
The answers reveal whether the 3PL engineered their infrastructure for operations like yours or whether they simply have space available.
The layout expertise embedded in a well-designed 3PL operation is invisible on a facility tour but determines cost-per-order for years.
Every pick path inefficiency, every replenishment bottleneck, every dock door conflict that occurs daily was either prevented or permitted by decisions made before the first box moved.
The engineering that happened before you arrived is what makes the best 3PL partnerships run smoothly at scale.